Industrial automation is the use of control systems — programmable logic controllers (PLCs), sensors, robots, and software — to operate production equipment with minimal human intervention. It improves manufacturing by making processes faster, more consistent, and more repeatable, which raises throughput, cuts defects and waste, improves worker safety, and gives plant managers real-time visibility into their lines. Automation does not replace skilled workers; it moves them from repetitive manual tasks to supervision, maintenance, and continuous improvement.
What Is Industrial Automation?
In plain language, industrial automation means letting machines, sensors, and controllers do the work that people used to do by hand. Instead of an operator watching a conveyor and pressing a stop button when products back up, a sensor detects the condition and a controller acts on it automatically — in milliseconds, every time, without fatigue.
Automation is not a single technology. It is a spectrum that ranges from a single automated valve on a filling line, to a motorized conveyor that moves product between stations, to a robotic cell, to a fully integrated plant where every machine reports live data to a central control room. Most factories sit somewhere in the middle of that spectrum, and most can move further along it without rebuilding their entire operation.
A common misconception is that automation replaces workers. In practice, it complements them. Machines are excellent at repetitive, heavy, and hazardous tasks; people remain essential for judgment, setup, quality decisions, maintenance, and improvement. A well-automated line still needs operators, electricians, and engineers — but their time is spent on higher-value work than pushing and watching product move.
How Does Industrial Automation Work?
Every automated system, from a simple temperature controller to a full robotic line, operates on the same principle: a closed loop with three parts.
- Sensor — measures a condition: product presence, position, temperature, pressure, speed, or count.
- Controller — receives the sensor signal, compares it against a desired value (the setpoint), and decides what to do.
- Actuator — executes the decision: starting or stopping a motor, opening a valve, diverting a product, or triggering a robot.
The controller continuously reads new sensor data, so the system corrects itself as conditions change. That feedback loop is the heart of automation.
A concrete example on a production line. Picture a bottling line with a conveyor feeding a filling station:
- A photo-eye sensor detects empty bottles arriving on the conveyor systems and counts them as they pass.
- It sends each count to a PLC, which compares the flow against the filler’s speed.
- If bottles bunch up, the PLC signals the conveyor motor drive to slow down or stop; if gaps appear, it speeds the conveyor back up.
- A second sensor downstream confirms every bottle reached the filler, and the PLC triggers a rejection gate when a defect is detected.
- An HMI screen shows the operator live line status and lets them change the target speed.
Nothing about this requires replacing the line. Adding sensors, a PLC, and a variable-speed drive converts a manual operation into a controlled, automated one.
How Automation Improves Manufacturing
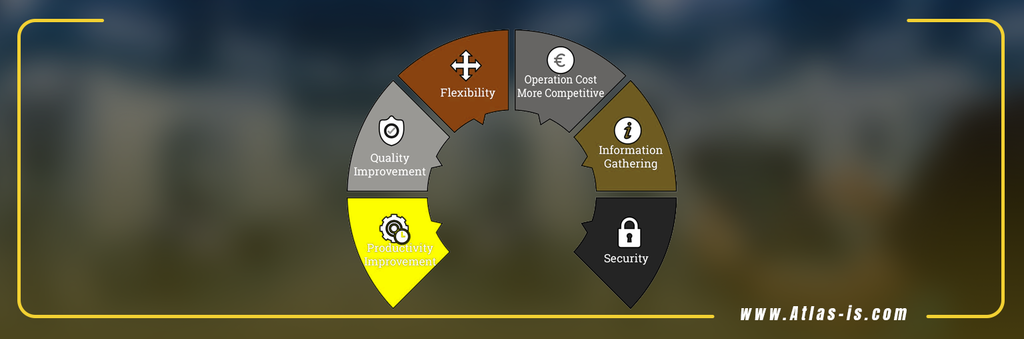
Automated production lines deliver improvements through clear mechanical and logical mechanisms — not magic. Understanding those mechanisms matters because it tells you where automation will actually pay off in your factory. It is also one of the most direct ways to improve production line efficiency, so the two goals should be planned together.
Quality and Consistency
An automated system performs the same sequence with the same parameters every single cycle. It does not tire, lose concentration, or vary between shifts, so the product leaving the line at 3 a.m. matches the product from 9 a.m. That repeatability reduces defects caused by human variation. In-line sensors and machine-vision cameras go further: they inspect every unit as it passes, catching problems at the point of occurrence rather than after the batch is finished, which cuts rework and scrap.
Throughput and Productivity
Machines cycle faster than people on repetitive tasks and do not need breaks, shift handovers, or rest pauses. Equipment also becomes more productive because material flow is orchestrated: conveyors keep machines fed, sensors prevent jams before they happen, and programmable setpoints make changeover between products faster. Throughput rises not only because individual steps are faster, but because the whole line stops losing time waiting for the next unit to arrive.
Safety
Automation removes people from the tasks most likely to injure them: heavy lifting, repetitive strain, and working near moving machinery, heat, or chemicals. When people do need to enter a machine’s working area, interlocks and light curtains detect their presence and stop the equipment automatically. Less manual material handling also means fewer accidents from carrying, pushing, and forklift traffic. The mechanism is simple: fewer humans in the hazard zone means fewer human injuries.
Cost Reduction
Automation reduces cost through four mechanisms, and only these:
- Labor — hours spent on repetitive handling shrink as machines take over those tasks, so the same output needs fewer direct labor hours per unit.
- Waste and rework — consistent processes produce fewer defective units, so less material is scrapped.
- Energy — variable frequency drives run motors at exactly the speed required instead of full speed always, and driven equipment stops when the line stops, so no energy is consumed idling.
- Maintenance — controlled starts and stops reduce mechanical stress on equipment, and monitoring catches problems early.
Note the honest side: automation also adds capital cost, control-system maintenance, and some energy use for electronics. That is why the savings must be quantified against your own baseline before you invest — which is covered in the considerations below.
Data and Decision-Making
Once sensors and controllers are in place, the line generates data: throughput, downtime, cycle times, rejection counts, and machine condition. Operators and managers see this in real time instead of discovering a problem at the end of the shift. The same data enables predictive maintenance — vibration and temperature sensors on motors and drives show degradation well before failure, so repairs are scheduled instead of suffered. Aggregated into a single number, these measurements form the Overall Equipment Effectiveness (OEE) metric — availability multiplied by performance multiplied by quality — which is the standard way plant managers track how fully a production line is working.
Connecting these systems to business software follows recognized frameworks: ISA-95 (published internationally as IEC 62264) is the standard for integrating enterprise systems with manufacturing control, defining how data flows between the plant floor and the ERP system. And because networked automation opens new attack surfaces, IEC 62443 is the international standard series for industrial automation cybersecurity, structuring networks into zones and specifying security levels for control systems.
Types of Industrial Automation
There is no single “right” kind of automation. The choice depends on production volume, product variety, and how often the line changes over.
| Type | How it works | Best for |
|---|---|---|
| Fixed (hard) automation | Dedicated equipment engineered for one specific sequence of operations; the sequence is built into the machinery and rarely changed | High-volume, low-variety products — filling, bottling, and packaging lines |
| Programmable automation | A programmable controller (PLC or CNC) changes the operating sequence when the product batch changes | Batch production — food recipes, molded parts, machining jobs with limited variety |
| Flexible automation | Equipment reconfigures itself automatically between products with minimal downtime | Mixed products in continuous flow — robotic cells and assembly lines with frequent changeovers |
| Integrated automation | All systems — PLCs, SCADA, robots, conveyors, and business software — operate under one control and data architecture, following the ISA-95 model | Large facilities where production must be coordinated end-to-end |
In practice (a reasonable assumption for the Egyptian market), most factories run a combination: fixed conveyor elements, programmable PLC control, and a few flexible robotic or automated stations. You do not need full integrated automation to benefit — the highest returns often come from targeted programmable automation at the bottleneck.
Core Components and Technologies
These are the building blocks of almost every automated production line. Each is defined here so the terminology is clear.
PLC (Programmable Logic Controller)
An industrial computer that runs the control logic for a machine or process. It reads sensor inputs, executes its programmed logic, and drives outputs such as motors and valves — making decisions in real time, reliably, and in harsh factory environments.
SCADA (Supervisory Control and Data Acquisition)
A software system that supervises the whole plant from above. It collects data from many PLCs, displays it on operator dashboards, manages alarms, and stores history so managers can analyze performance. The PLC controls; SCADA supervises.
HMI (Human-Machine Interface)
The screen and control panel operators use to interact with the system — viewing live status, changing setpoints, and acknowledging alarms. An HMI is the window into the automation.
Sensors and Machine Vision
The sensory layer of the loop. Sensors detect presence, position, temperature, pressure, and count; machine-vision cameras inspect products for defects, verify labels, and guide robots. Together they give the controller accurate information about what is actually happening on the line.
Robotics
Programmable manipulators — articulated arms, gantry robots, and delta robots — that move, assemble, weld, pack, and palletize with consistency and speed. Robots are the most visible form of automation and typically the most flexible.
Conveyors and Material Handling
The transport layer that moves products between stations in a controlled, steady flow. As outlined in our guide to conveyor systems, the right conveyor design determines whether the rest of the automation ever gets the chance to work at full speed — a starved machine cannot produce.
IIoT and MES
The Industrial Internet of Things (IIoT) connects machines, sensors, and controllers to each other and to analytics platforms, enabling condition monitoring and predictive maintenance. The Manufacturing Execution System (MES) sits at the operations level: it tracks production orders, routing, quality results, and equipment status in real time, bridging the gap between the shop floor and the ERP system.
The control layer — PLCs, SCADA, and HMI — is exactly the kind of engineering delivered under automation and electrical solutions projects, including electrical panels and system integration.
Industrial Automation in the Egyptian Market
Observed across Egyptian manufacturing, the industrial base spans food and beverage, pharmaceuticals, chemicals, packaging, building materials, and textiles — high-volume, quality-critical sectors where automation is already standard in modern plants and where competitive pressure is pushing older facilities to catch up. For these factories, automation is usually considered not as a green-field project but as an upgrade path for existing operations.
Several patterns are common in the local market:
- Retrofitting over replacement. Most investment goes into modernizing lines that already run: adding sensors and PLCs to manual stations, motorizing conveyor sections, and upgrading control panels. This preserves the original capital investment in machines and avoids the cost of starting over. A retrofit is typically staged line by line.
- Skills and training. Automation changes the workforce’s needs: operators must read HMIs and respond to alarms, and maintenance teams need control-system troubleshooting skills. Training is not a luxury add-on — it is a condition for getting the expected benefits from the equipment.
- Spare parts and local supply. Control components, drives, sensors, and conveyor parts fail eventually, and production cannot wait for long import lead times. Factories that plan spare-part continuity with suppliers who fabricate and stock locally keep downtime under control.
The general pattern is pragmatic: Egyptian manufacturers automate where the mechanism is clear — material handling, bottleneck processes, and quality-critical steps — rather than chasing full automation for its own sake.
What to Consider Before Automating a Production Line
Production line automation projects fail when they start from technology instead of from the problem. A practical sequence looks like this:
- Start with the bottleneck. Find the single stage that limits line output — the packaging station that cannot keep up, or the manual transfer that starves the next machine. Automating the bottleneck delivers more output per pound invested than automating a station that already runs ahead of demand.
- Measure a baseline. Record current throughput, downtime, defect rates, and labor hours per unit for at least a few weeks. Without a baseline you cannot prove the project worked, and you cannot calculate payback honestly.
- Frame ROI around specific mechanisms. Estimate the savings from the mechanisms described above — labor hours removed, scrap reduced, output gained — and compare them to the full project cost, including controls, installation, training, and spares. ROI is a calculation on your numbers, not an industry average.
- Pilot on one line. Prove the approach on a single production line at a contained cost, measure the result against the baseline, then replicate. Pilots de-risk the investment and give maintenance and operators experience before wider rollout.
- Plan integration and training early. Check how new controls will communicate with existing equipment, and plan data integration with production or ERP systems under the ISA-95 model. If the line will connect to company networks, apply IEC 62443 cybersecurity practices to protect control systems. Training must be scheduled before the line goes live, not after.
- Budget for maintenance and spare parts. PLCs, sensors, drives, and conveyor components need spares and skilled people to keep them running. A machine that cannot be repaired quickly converts a modern line into an expensive source of downtime.
How Atlas Industrial Solutions Can Help
Atlas Industrial Solutions designs, builds, installs, and maintains industrial automation systems across the full lifecycle of a production line, which is what makes automation projects achievable for Egyptian factories of any size:
- Material handling and conveying — custom-designed conveyor systems matched to your product, layout, and speed requirements, from single belt conveyors to complete multi-stage transport.
- Automation and electrical solutions — control systems, PLCs, SCADA, robotics, and electrical panels engineered to integrate with your existing equipment.
- Production line installation — turnkey production line installation from design through build, testing, and commissioning, carried out to minimize disruption to your operations.
- Spare parts fabrication and supply — locally fabricated and supplied spare parts that keep your line running without waiting on long import lead times.
- Maintenance — ongoing support that protects the availability of both new and existing equipment.
The company’s working model is straightforward: meet and agree on the problem, develop the concept, design and build the solution, and install it — with post-install training included so your operators can run and maintain the system themselves.
If you want to assess whether automation makes sense for your bottlenecks, or to discuss a specific line, talk to the team via the request for quotation page with your product details and production requirements.
FAQ
How much does industrial automation cost, and how fast is the payback?
Costs vary widely with scope — a sensor-and-controller retrofit on one line costs far less than a new robotic cell. Payback depends on the mechanisms you capture: labor hours, scrap, throughput, or maintenance expense. Define a baseline, project the specific savings, and evaluate payback against those numbers rather than industry averages.
Can I automate an existing production line without replacing it?
Yes. Most automation projects are retrofits: adding sensors, PLCs, drives, and motorized conveyor sections to equipment you already run. This preserves your capital investment and avoids replacing healthy machines. A staged retrofit starting at the bottleneck delivers measurable gains with lower cost and less risk than building a new line.
Will automation cause downtime during installation?
Installation is usually phased to protect production: work is scheduled in planned stoppages, weekends, or changeover windows, with commissioning and testing completed before full handover. A well-managed integrator sequences the work so partial operation continues where possible. The goal is minimal interruption, executed around your production calendar.
Do operators need to be retrained when a line is automated?
Yes. Operators shift from repetitive handling to supervising the automated line: reading HMIs, responding to alarms, and managing changeovers. Maintenance teams need basic control-system skills. Training should be part of the project scope, covering operation, troubleshooting, and safety before the line goes live — not an afterthought once problems appear.
Is automation worth it for a small or medium factory?
Often, yes — provided it targets the right processes. Small and medium factories rarely need plant-wide automation; they need the bottleneck automated, a few sensor-and-PLC upgrades, or conveyorized material handling. Starting small keeps the investment contained and lets you measure real results on one line before scaling to the rest of the factory.
What is the difference between a PLC and SCADA?
A PLC controls a specific machine or process in real time — reading sensors and driving outputs within milliseconds. SCADA sits above PLCs: it collects data from many controllers across the plant, displays it on operator dashboards, manages alarms, and builds history for analysis. In short, the PLC executes; SCADA supervises.
Does industrial automation replace jobs?
Automation changes work more than it eliminates it. Repetitive, heavy, and hazardous tasks move to machines, but every automated line still needs operators, programmers, electricians, and maintenance technicians — in many cases more highly skilled ones. The practical question for a plant manager is how to retrain and redeploy people, not whether jobs vanish entirely.
Which industries benefit most from industrial automation?
The highest returns appear in high-volume, quality-critical, or safety-sensitive processes: food and beverage, pharmaceuticals, packaging, chemicals, and building materials all use automation widely. But any line that moves product between stages — assembly, filling, sorting, packing — benefits from conveyor-based material handling and basic control, regardless of industry.
Conclusion
Industrial automation is not an all-or-nothing decision. It is a spectrum of technologies — sensors, controllers, conveyors, robots, and software — that work together to make manufacturing faster, more consistent, safer, and more visible. The benefits are real, but they come from specific mechanisms: repeatability, continuous operation, physical separation of people from hazards, and data. Before you invest, find the bottleneck, measure a baseline, and calculate payback from your own numbers.
For most Egyptian factories, the practical path is a staged retrofit: automate the constraint, prove the results on one line, then expand. When you are ready to evaluate your production line — whether that means conveyorized material handling, control-system upgrades, a full production line installation, or simply planning spare parts and maintenance — an experienced partner makes the difference between a technology purchase and a measurable productivity gain. Start the conversation with a request for quotation, and tell the team what your line produces and where it bottlenecks; the engineering conversation begins from there.